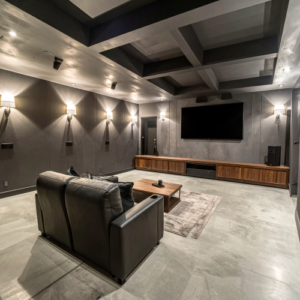
The Floor Your Man Cave Deserves: Why Bare Concrete Doesn’t Cut It
Blog The Floor Your Man Cave Deserves: Why Bare Concrete Doesn’t Cut It A man cave is where you watch the game, host poker night,

Raw concrete in an industrial environment degrades faster than almost any other application. Heavy loads, chemical exposure, thermal cycling, and constant abrasion create conditions that break down an unprotected slab from multiple directions simultaneously. Here's what that actually costs you.
Unsealed concrete sheds fine particulate constantly — settling on machinery, contaminating products, clogging filters, and degrading air quality. In some industries that's a compliance issue, not just a cleanliness one.
Oils, hydraulic fluid, solvents, fuel, and cleaning chemicals soak permanently into unprotected concrete. Once they're in the slab they can't be fully removed — creating slip hazards and accelerating surface deterioration.
Forklift traffic, pallet jacks, and heavy rolling equipment wear down uncoated concrete over time — creating uneven surfaces, cracks, and trip hazards that create OSHA exposure and increase incident risk.
An unsealed industrial floor absorbs everything and releases nothing. Your team spends more time and resources on a floor that never looks clean regardless of the effort.
A deteriorating floor is one of the first things a client, partner, or inspector sees. It signals operational neglect regardless of how well everything else is running.
A professional industrial coating system addresses every one of these problems in a single installation — and Outback's system is backed for the life of the floor.
Outback installs ArmorCore™ — a commercial and industrial-grade polyurea coating system that is a fundamentally different product from the residential coatings most contractors apply. Applied at proper film thickness over a correctly prepared surface, it's engineered for real industrial environments.
Engineered to handle forklift axle loads, pallet rack legs, and heavy machinery without cracking, indenting, or losing adhesion.
Formulated to stand up to fuels, hydraulic fluids, caustic cleaners, oils, and process chemicals — stopping them at the surface where they can be managed, not absorbed.
Eliminates concrete dust, resists microbial growth, and can be cleaned efficiently with standard industrial equipment. No more losing the battle against an absorbing surface.
Color-coded traffic lanes, hazard zones, pedestrian walkways, and equipment staging areas applied as part of the coating system — not painted on top afterward.
Shark-grip aggregate embedded in the topcoat creates a permanent slip-resistant profile — critical in industrial environments where wet floors and spills are an operational reality.
Industrial floor failure has real consequences — downtime, safety risk, repair cost, and operational disruption. Outback backs every qualifying ArmorCore™ industrial installation with a Lifetime Transferable Coating Warranty including 10-year labor and materials on covered failures.
"Ask any contractor you're evaluating to show you their warranty in writing — including whether it covers both labor and materials. We put ours in the contract before the install begins."
Free facility assessment. We evaluate your slab, spec the right system for your environment, and give you an exact price before any work begins. No pressure. No obligation.
(260) 600-7600Industrial floors don’t get a day off. They carry forklifts, absorb chemical spills, take the impact of dropped equipment, and endure the constant grinding of heavy machinery, shift after shift, year after year. Bare concrete was never engineered to handle that kind of sustained punishment without breaking down, and when an industrial floor starts failing, it doesn’t just look bad, it becomes a safety issue, a maintenance burden, and an operational liability.
Outback Concrete Coatings installs professional-grade industrial floor coating systems across Fort Wayne and Eastern Indiana, engineered for real working conditions, applied by trained technicians who understand what industrial environments actually demand, and backed by a lifetime warranty that means something in a facility where floor failure has real consequences.
Raw concrete in an industrial environment degrades faster than almost any other application. The combination of heavy loads, chemical exposure, thermal cycling, and constant abrasion creates a set of conditions that break down an unprotected slab from multiple directions simultaneously.
Here’s what uncoated industrial concrete costs you, beyond the obvious:
Concrete dust — Unsealed concrete sheds fine particulate constantly. In a manufacturing or distribution environment, that dust settles on machinery, contaminates products, clogs filters, and degrades air quality for everyone working in the space. It’s not just a cleanliness issue, it’s a maintenance issue and in some industries a compliance issue.
Chemical penetration — Industrial fluids, oils, hydraulic fluid, solvents, cleaning chemicals, fuel, soak into unprotected concrete permanently. Once they’re in the slab, they can’t be fully removed, they create slip hazards, and they accelerate surface degradation. Sealed concrete stops them at the surface where they can be managed.
Surface deterioration — Heavy forklift traffic, pallet jacks, and rolling equipment wear down the surface of uncoated concrete over time, creating uneven surfaces, cracks, and trip hazards that create OSHA exposure and increase the risk of equipment and vehicle incidents.
Maintenance burden — Trying to keep an unsealed industrial floor clean is a losing battle. The porous surface absorbs everything and releases nothing, which means your maintenance team spends more time and resources on a floor that never looks clean regardless of the effort.
Reduced facility value — The condition of your facility floor is one of the first things a prospective client, partner, or inspector sees when they walk in. A deteriorating floor signals operational neglect regardless of how well everything else is running.
A professional industrial coating system addresses every one of these problems in a single installation, and our system is backed for life.
For heavy industrial environments, high-build epoxy coating is the system of choice, and it’s what Outback installs across Fort Wayne’s warehousing, manufacturing, and distribution facilities. Industrial-grade epoxy is a fundamentally different product from the residential epoxy systems that give the material a mixed reputation. Applied at proper film thickness over a properly prepared surface, it delivers:
Best suited for: Warehouses and distribution centers, manufacturing facilities, food and beverage processing, automotive service and manufacturing, chemical storage and processing facilities, institutional and municipal maintenance facilities.
Three active markets across Indiana and Ohio. Local crews, same-day installs, no long hauls.
Northeast Indiana · Headquartered at 3909 Fourier Dr, Suite C
Serving Van Wert and surrounding areas · Dayton location coming soon
Blog The Floor Your Man Cave Deserves: Why Bare Concrete Doesn’t Cut It A man cave is where you watch the game, host poker night,
Blog Find us at the DeKalb County Fair And enter to win a free 500 Sq. Ft. Garage Floor “America’s Family Reunion” is back in
Blog More Than Garage Floors: Everywhere Outback Concrete Coatings Shows Up Here’s a full look at where we work, whether it’s in your home, your
Blog The Armor Core System™: What It Is, and Why It Outperforms a Standard Epoxy Floor Here’s what’s in it, why the layered approach outperforms
Blog Rubber Vs. Polyaspartic: Which is right for your Pool Deck? Thinking about rubber surfacing for your pool deck or patio? See how it compares
Real Jobs, Real Surfaces, Real Results: Our Featured Projects So Far We’re kicking off a new Featured Projects series to show the community exactly what